AirLeak
What your compressed-air leaks cost, measured at the compressor every weekend
Measures how hard your compressors work when the plant is idle and turns it into a weekly dollar figure for leaks, so you know when a leak hunt is worth doing and whether the last one held.
- Who buys it
- The plant manager or maintenance lead at a small plant with 1–3 screw compressors of any brand; compressed-air service shops resell it.
- Why it pays
- Example 50 hp plant idling at 40% load: about $9,000/yr of leaks; bringing it to 15% is worth about $5,600/yr (est.).
- Target price
- $590 kit + $19/site/month; extra compressor CT $79; handheld probe $179 (target)
- First-minute wow
- A Monday email that says "Idle air last weekend: $175, $9.1k/yr pace, up 12% since your September survey", with the method and its confidence shown.
What the research found
And how this design answers it
- MEMS mics can't locate leaks in a noisy plant at 80 kHz → no fixed acoustic array; leak quantity is measured at the compressor (current) and header (pressure)
- Atlas Copco SMARTLINK is free for Atlas machines → brand-agnostic clamp-on retrofit for any compressor, including old relay-controlled ones
- Leak savings were estimates → the weekend figure is the DOE/CAC load-unload measurement (T/(T+t)), run automatically every weekend
- Handheld ultrasonic detectors cost $3,495+ → optional $179 40 kHz heterodyne probe for walking a valve bank at 1–3 m
- Flow meters ($625+) give cfm, not dollars → works without one; accepts a 4–20 mA meter for VSD compressors
- Surveys are one-off → before/after reports prove a repair day paid and alert when leaks creep back
Use case
The weekend leak bill
Plant managerMaintenance techCompressed-air service shop
- 01Trigger: Saturday to Monday, no production, the compressor keeps loading and unloading
- 02Detection: the node times every loaded and unloaded interval from the current clamp; the cloud computes 40% idle load ≈ 84 cfm
- 03Alert: Monday email with $175 this weekend, $9.1k/yr pace and a 12-week trend
- 04Action: the tech walks the plant with the probe, tags 20 leaks, fixes 15; next weekend's report shows the drop
Outcome: Idle load from 40% to about 15%: about $5,600/yr saved (est.)
How it works
Architecture
- 01
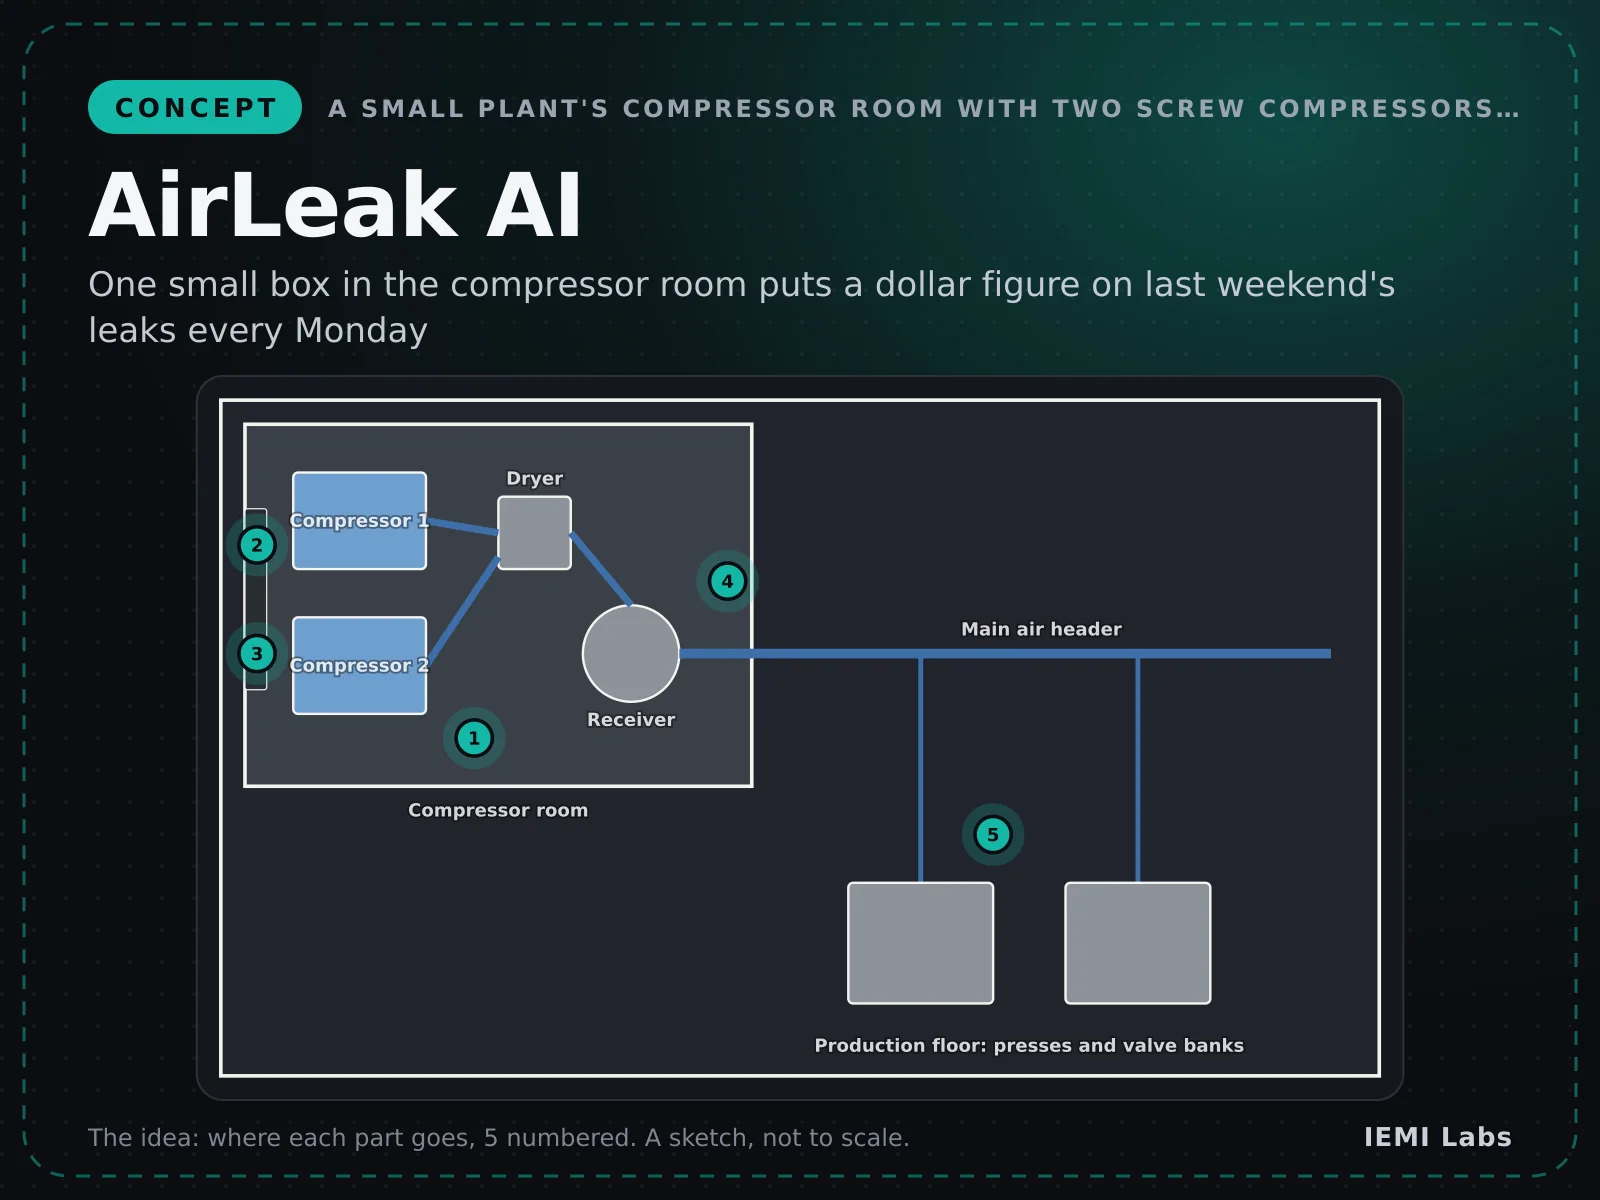
Sense: 200 A split-core CT per compressor (0.333 V), 0–200 psi header transducer, optional 4–20 mA flow meter
- 02
Decide (node): ESP32-S3 + ADS131M04 classify each compressor as off, unloaded, loaded or VSD every second
- 03
Send: 60 s telemetry and state events over MQTT/TLS on Wi-Fi, 7-day flash buffer
- 04
Decide (cloud): quiet-window detection, leak % by load/unload, drawdown or flow method, kW and $
- 05
Tell: Monday report, web dashboard, phone app with probe survey and leak list
Hardware
Real parts, buyable today
Bill of materials: about $392 per node kit at qty 1 (transducer $273), about $215 at qty 60 (est.); probe about $30 of parts.
| Block | Part | Why this part |
|---|---|---|
| MCU + Wi-Fi | ESP32-S3-WROOM-1-N8R8 | Wi-Fi, PSRAM for a 7-day buffer, $6.13 |
| ADC | TI ADS131M04 24-bit 4-ch simultaneous | Reads 0.333 V CTs and pressure directly |
| Current | Magnelab SCT-1250-200 split-core CT | Clamp-on, low-voltage output, up to ~150 hp at 460 V, $44.52 |
| Pressure | Honeywell PX3AN2BS200PSAAX 0–200 psi | Industrial 1/4" NPT, 0.5–4.5 V; drawdown tests |
| Probe | Murata MA40S4R + NXP SA612A heterodyne + ESP32-C3 | 40 kHz leak hiss to headphones plus BLE level, for under $40 of parts |
Mechanical
Printable CAD
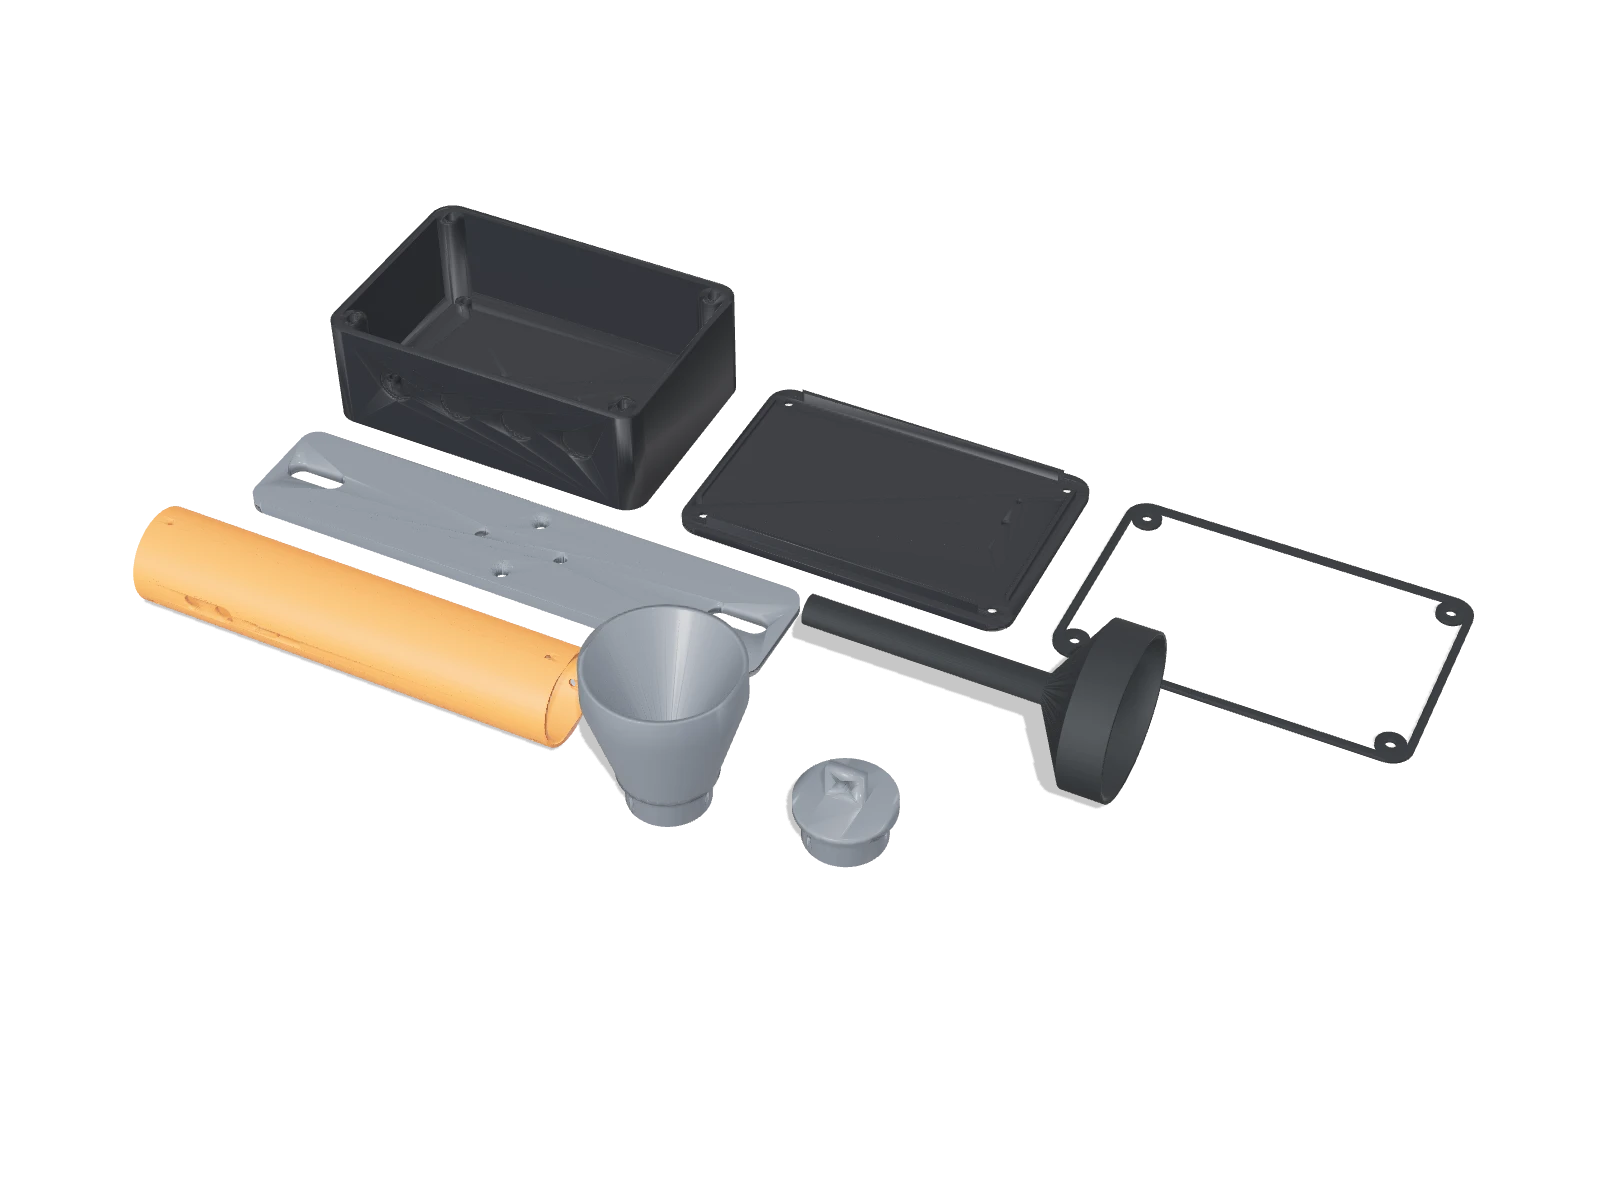
8 parts, generated from code and checked as closed solids. Pick a part to inspect it, or download the STL files to print.
See the CAD parts render
Loading the CAD…
Real CAD · drag to rotate · scroll to zoomReal CAD · swipe sideways
Bought hardware fitted inside this part (checked in the CAD: nothing collides with the plastic)
- Node basenode-base.stl · ASA, black
- Node lidnode-lid.stl · ASA, black
- Node gasketnode-gasket.stl · TPU 95A
- Wall / strut mount platemount-plate.stl · ASA or PETG
- Probe bodyprobe-body.stl · PETG, orange
- Probe horn (40 kHz receiver seat)probe-horn.stl · PETG
- Probe end cap with lanyard lugprobe-cap.stl · PETG
- Pinpoint focus tubefocus-tube.stl · TPU 95A
Open risks we are working on
- Idle demand that isn't leakage (drains, dryer purge, timers) inflates the figure; needs tagging and a zone-off test
- VSD compressors: current-to-flow is only ±20% without a flow meter or drawdown test
- Pressure transducer cost at qty 1 ($273) squeezes kit margin until volume or a cheaper part is qualified
- Plant IT may block Wi-Fi; the LTE-M variant is not designed yet
- MA40S4R receiver is not for new designs; the probe needs a second source
Design stage only: nothing on this page is for sale. Specifications and prices are targets.